KSA Industrial Automation Company provides HMI development in Saudi Arabia for plants that want operators to see abnormal situations early and act on them correctly. We design and build screens, navigation and alarms on Siemens WinCC, Rockwell FactoryTalk View and Schneider panels, so that one glance at a page shows what the process is doing and what needs attention.
What you receive: a written proposal with the screen list, platform, alarm approach and programme within one working day of receiving your P&IDs, I/O list or existing screens. Request a quotation
HMI development: screens, alarms and platforms
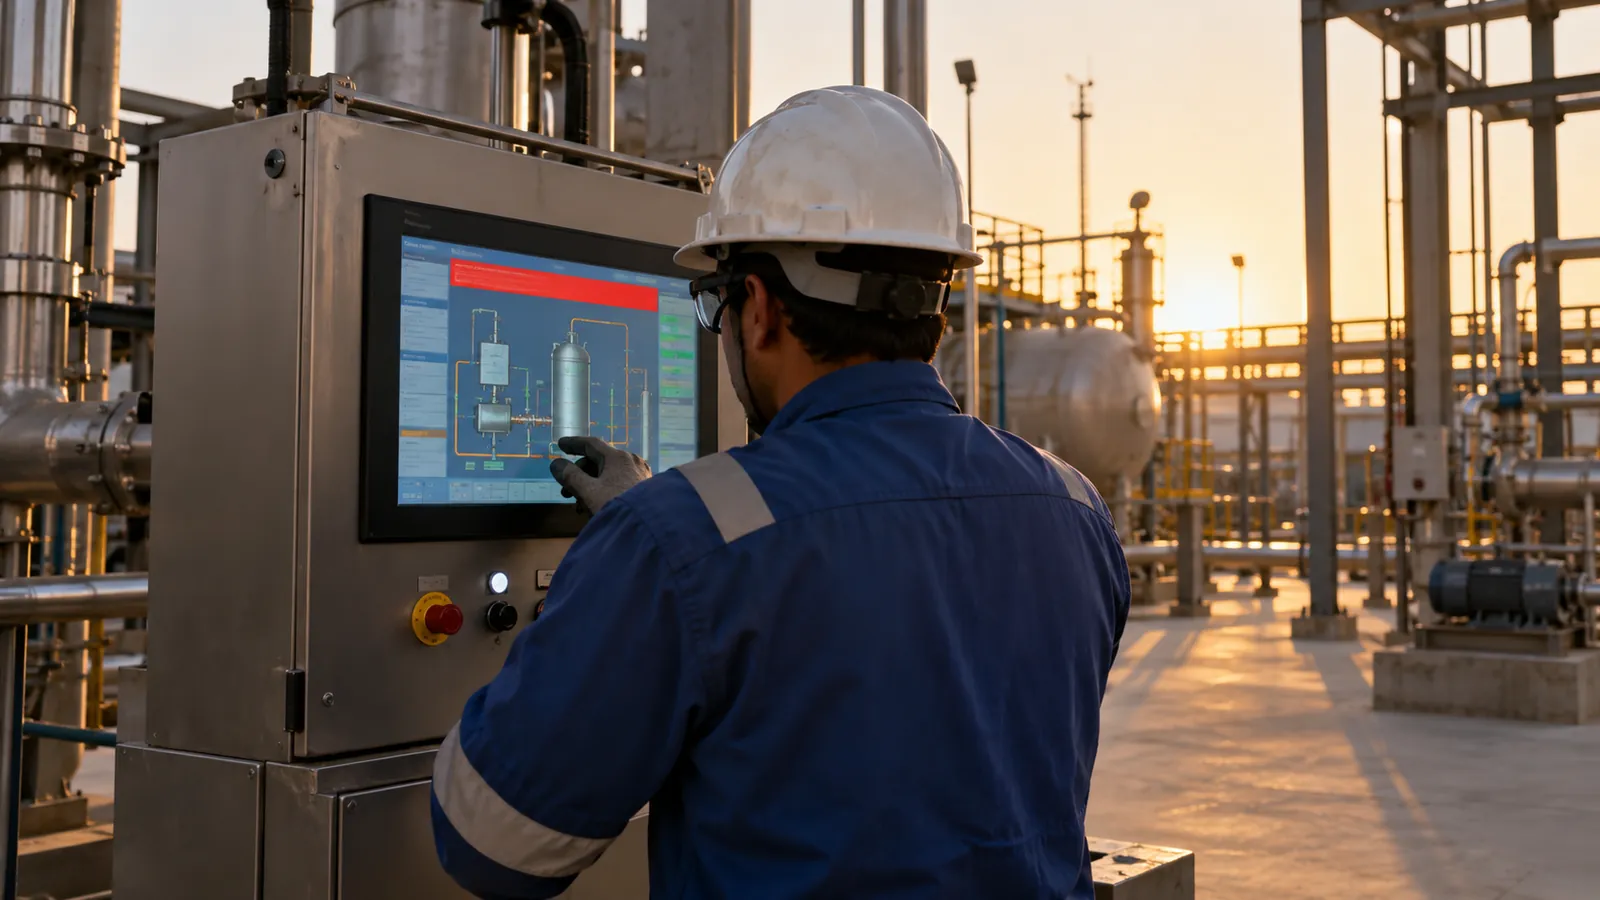
An HMI is the operator's only window into the process. Poorly designed screens hide trends, flood the operator with alarms and slow the response to a real upset. Our screens follow ISA-101 principles: restrained colour, grey process graphics, colour reserved for abnormal states, and a consistent navigation tree.
| Item | Platforms / range | Standard | Typical duration |
|---|---|---|---|
| Siemens HMI | WinCC Comfort and WinCC Unified | ISA-101 principles | 1–4 weeks |
| Rockwell HMI | FactoryTalk View | ISA-101 principles | 1–4 weeks |
| Schneider HMI | Vijeo and EcoStruxure Operator Terminal Expert | ISA-101 principles | 1–4 weeks |
| Alarm design | Priorities, set points, deadbands, shelving and suppression rules | ISA-18.2 where relevant | Included with screen design |
| Screen set | Overview, area, equipment faceplate, trend, alarm and diagnostics pages | Your plant style guide or ours | Per screen count |
| Tag and faceplate library | Reusable objects linked to PLC data blocks | IEC 61131-3 data structure | Included |
Duration scales with the number of screens and equipment types. A single skid panel is a matter of days; a multi-area plant with faceplates for every motor, valve and loop takes the full range.
What is an HMI for a PLC?
An HMI, or human-machine interface, is the screen through which people read and command a PLC. The PLC runs the logic and holds the data. The HMI displays values, accepts operator commands such as start, stop and set point changes, and shows alarms. Local panels sit beside a machine. Larger plants use SCADA stations that collect many controllers into one view, which we cover under SCADA integration.
Can an HMI work without a PLC?
An HMI needs a data source, but that source does not have to be a PLC. Panels can read from drives, meters, instruments and gateways over Modbus, OPC UA or Ethernet protocols. Without any controller, the screen only shows internal tags and has no process to display. In most plants the PLC remains the data source, because it also enforces the interlocks that protect equipment.
How are HMI screens designed, built and handed over?
- Brief. You share P&IDs, the I/O list, existing screens and any plant graphics standard.
- Screen plan. We propose a navigation tree and a screen list, and agree the colour and symbol rules with you.
- Alarm review. We list every alarm with its cause, consequence, priority and operator action, then remove the ones that do not need a response.
- Build. Faceplates and pages are built once and reused, which keeps behaviour identical across equipment.
- Simulation. Operators or your engineers click through the screens against simulated data before anything reaches site.
- Site commissioning. We connect to live signals, check each indication against the field and correct scaling and units.
- Documentation. You receive the project archive, the alarm list and a short operator guide.
- Support. Changes after handover follow a simple change record, remotely or on site.
Read the companion article on HMI alarm philosophy in how to write an HMI alarm philosophy for the reasoning behind step three.
Which HMI software do plants use most?
The software follows the controller. Siemens plants use WinCC through TIA Portal, Rockwell plants use FactoryTalk View, and Schneider plants use Vijeo Designer or EcoStruxure Operator Terminal Expert. Programming the panel in the same environment as the controller means shared tags, one backup and one skill set for your maintenance team. Our PLC programming and Siemens TIA Portal teams build the controller and the screens together.
Who we build operator screens for
KSA Industrial Automation Company has worked in Saudi Arabia since 1995 and is approved by Saudi Aramco, SABIC and the Royal Commission for Jubail and Yanbu. We have worked on projects for all three.
Our screens run on pump stations, water treatment plants, tank farms, compressor skids and production lines. Cement, food and plastics plants use them for line overviews and fault diagnostics. We take HMI projects in every region of Saudi Arabia, and remote support is available the same day.
HMI questions answered
Who provides HMI development in Saudi Arabia?
KSA Industrial Automation Company provides HMI development in Saudi Arabia from its Dammam base, covering WinCC, FactoryTalk View and Schneider panels. We have been active since 1995 and have worked on projects for Saudi Aramco, SABIC and the Royal Commission.
What affects the cost of HMI design?
The main factors are the number of screens, the number of equipment types needing faceplates, the alarm count, the panel or software licence, the languages displayed and the testing you require. A style guide supplied by you shortens the design stage. Send your P&IDs and I/O list and the proposal prices each factor.
How long does HMI programming take?
Most HMI projects take between one and four weeks. A single panel for one machine sits at the short end. A multi-area plant with equipment faceplates, trends and a full alarm review sits at the long end. Early approval of the screen plan saves the most time.
Can you redesign the screens on our existing system?
Yes. We review your current screens and alarm list, propose a cleaner navigation structure, rebuild the pages on your existing platform and test them offline. Operators keep the same data underneath, so the change is to presentation and alarms rather than to control logic.
Do you build screens for Arabic and English operators?
Yes. We build bilingual screens with text lists and language switching on the platforms that support it, and we test font, direction and layout on the actual panel. You confirm the translations, and we load them into the project.
What should I send to get a quotation?
Send your P&IDs, I/O list and any existing screens or screenshots. Tell us the panel size or software platform if it is fixed. We then issue a scoped quotation within one working day.
Looking for HMI development in Saudi Arabia? Send us your P&IDs, I/O list or existing screens and receive a quotation within one working day.
Email: inquiry@ksaindustrialautomation.com | Request a quotation