KSA Industrial Automation Company provides plastics factory automation in Saudi Arabia: PLC and HMI control for extruders, blown film, injection moulding cells, auxiliaries and packaging lines. PLC programming typically takes 2–6 weeks per system. Our controls hold temperature, pressure and speed tight, so scrap and restart time fall and the line stays on target.
What you receive: a written proposal per machine or line, setting out scope, duration and price, back within one working day of your machine list and I/O. Request a quotation
Plastics factory automation: what we deliver
| Scope | Platforms and range | Standard | Typical duration |
|---|---|---|---|
| Extruder zone control and drives | S7-1200/1500, CompactLogix, Modicon M340 | IEC 61131-3 | 2–6 weeks per system |
| Line HMI with recipe storage | WinCC Comfort/Unified, FactoryTalk View, Vijeo | ISA-101 | 1–4 weeks |
| Auxiliaries: dryers, loaders, chillers | S7-1200, Modicon M340, ABB AC500 | IEC 61131-3 | 2–6 weeks per system |
| Plant monitoring, downtime and OEE | WinCC, FactoryTalk, AVEVA, Ignition | OPC UA, Modbus TCP | 4–12 weeks |
| Machine data gateways and FAT/SAT | Profinet, Ethernet/IP, Modbus, MQTT | Project procedure | Per project schedule |
For plants that also run filling or wrapping, see our production line automation page.
How is an extruder controlled by a PLC?
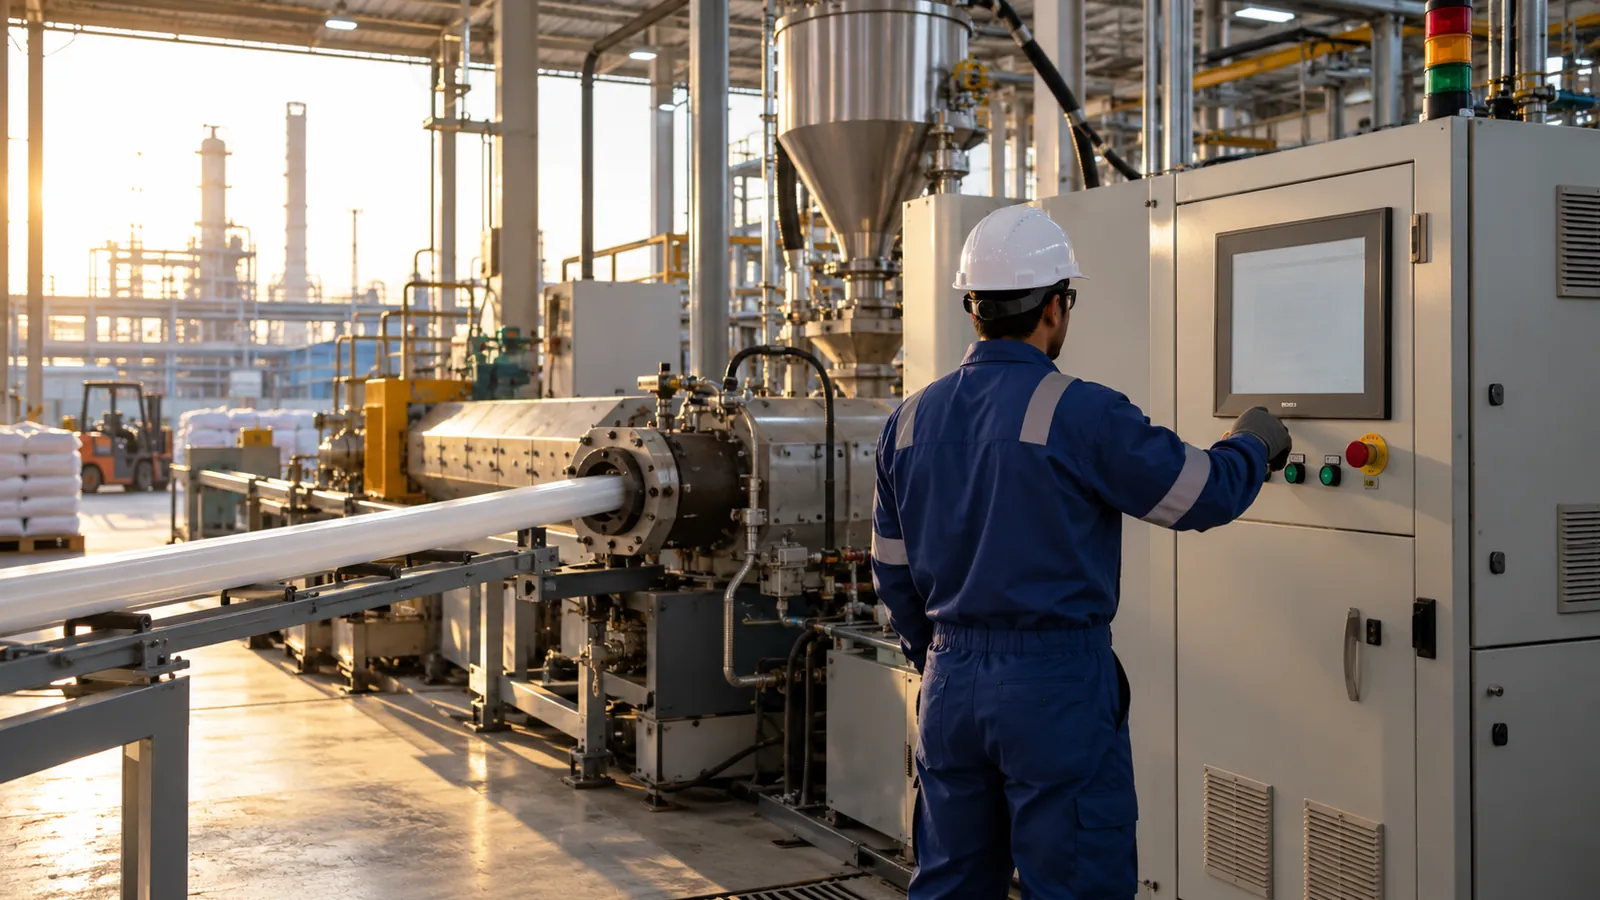
An extruder needs several loops held together. Barrel and die heaters run on PID zones with auto-tuning and over-temperature trips. Screw speed follows the drive, with melt pressure and motor load watched so a blocked screen is caught early. Take-off or haul-off speed ties to the screw so thickness stays stable. Recipes store every setpoint by product, so a restart reloads the full set and the first metres are usable.
What can we do about scrap and unplanned stops?
The first step is to measure them. We log each stop with a reason code chosen by the operator, link it to the machine state and show the top causes by shift. Many plants find that waiting for material, filter changes and cooling water temperature account for more lost time than any single breakdown. With that data you can fix the right problem, and the PLC alarms can warn of drift in melt pressure or chiller temperature before it costs a batch.
Can older machines share data with a central system?
Yes. Older injection and blow moulding machines often have a PLC with a serial or Ethernet port. We read it through a gateway into a plant SCADA over Modbus, Profinet, Ethernet/IP or OPC UA, and add counters for shots, cycle time and rejects. The machine's own control stays untouched, which protects its warranty and your production plan. See SCADA integration for platforms and reporting.
How does a plastics automation project run?
- You send an I/O list, drawings or a process description.
- We inspect the line or review documents, then issue the proposal.
- We write the functional design and screen layout with your production team.
- We programme and test on a bench before we reach the site.
- We install, check loops and commission in a planned stop. Support is remote the same day and on site within one working day in the Eastern Province.
- You receive backups, as-built code and operator training.
Where we work
Saudi plastics and packaging plants cluster in the Dammam industrial cities, Jubail, Riyadh and Jeddah. Our base is Al Shati District, Dammam, and we have worked on projects for Saudi Aramco, SABIC and the Royal Commission for Jubail and Yanbu. We are available for projects across Saudi Arabia. We hold ISO 9001, ISO 14001 and ISO 45001 certification. Many converters buy machines from several makers, so we give them one control standard across all of them.
Plastics factory automation questions
Who provides plastics factory automation in Saudi Arabia?
KSA Industrial Automation Company provides PLC, HMI and monitoring for extrusion, moulding and packaging plants from Dammam. It has operated since 1995 and is approved by Saudi Aramco, SABIC and the Royal Commission.
What affects the cost of extruder PLC control work?
The main factors are the number of heating zones and drives, I/O count, recipe handling, the platform, whether you need data reporting and how many machines are included. Make, model and a short list of faults help us price.
How long does a plastics line control upgrade take?
Time depends on I/O count, recipe needs and the stop windows you can spare. PLC programming typically takes 2–6 weeks per system and HMI 1–4 weeks. Most testing is done before the machine stops.
Can you retrofit controls on an imported extruder?
Yes. We replace obsolete controllers, add new HMI screens and tune heater zones to match your materials, and we keep the original drives and sensors where they are in good order.
Can you connect chillers and dryers to the main line?
Yes. We read their status over Modbus or discrete signals, show it on the line HMI and alarm on a temperature or dew point drift before it reaches the product.
What should we send for a quotation?
Send your I/O list, a machine list with make and model, and photos of the existing control cabinet. P&IDs or a short process description also let us scope the auxiliaries correctly.
Need plastics factory automation in Saudi Arabia? Send us your machine list, I/O list and cabinet photos, and get a quotation within one working day. Email: inquiry@ksaindustrialautomation.com | Request a quotation