KSA Industrial Automation Company provides compressor control system engineering in Saudi Arabia: PLC logic, HMI and SCADA interfaces for air compressors, gas compressors and packaged skids. We write the sequencing, protection and communication layers, test them at the packager's yard or in our Dammam office, and commission them on your site.
What you receive: a written proposal with the control narrative, I/O scope, communication interface, test plan and schedule within one working day of receiving your I/O list, P&ID or functional description. Request a quotation
What does a compressor control system do?
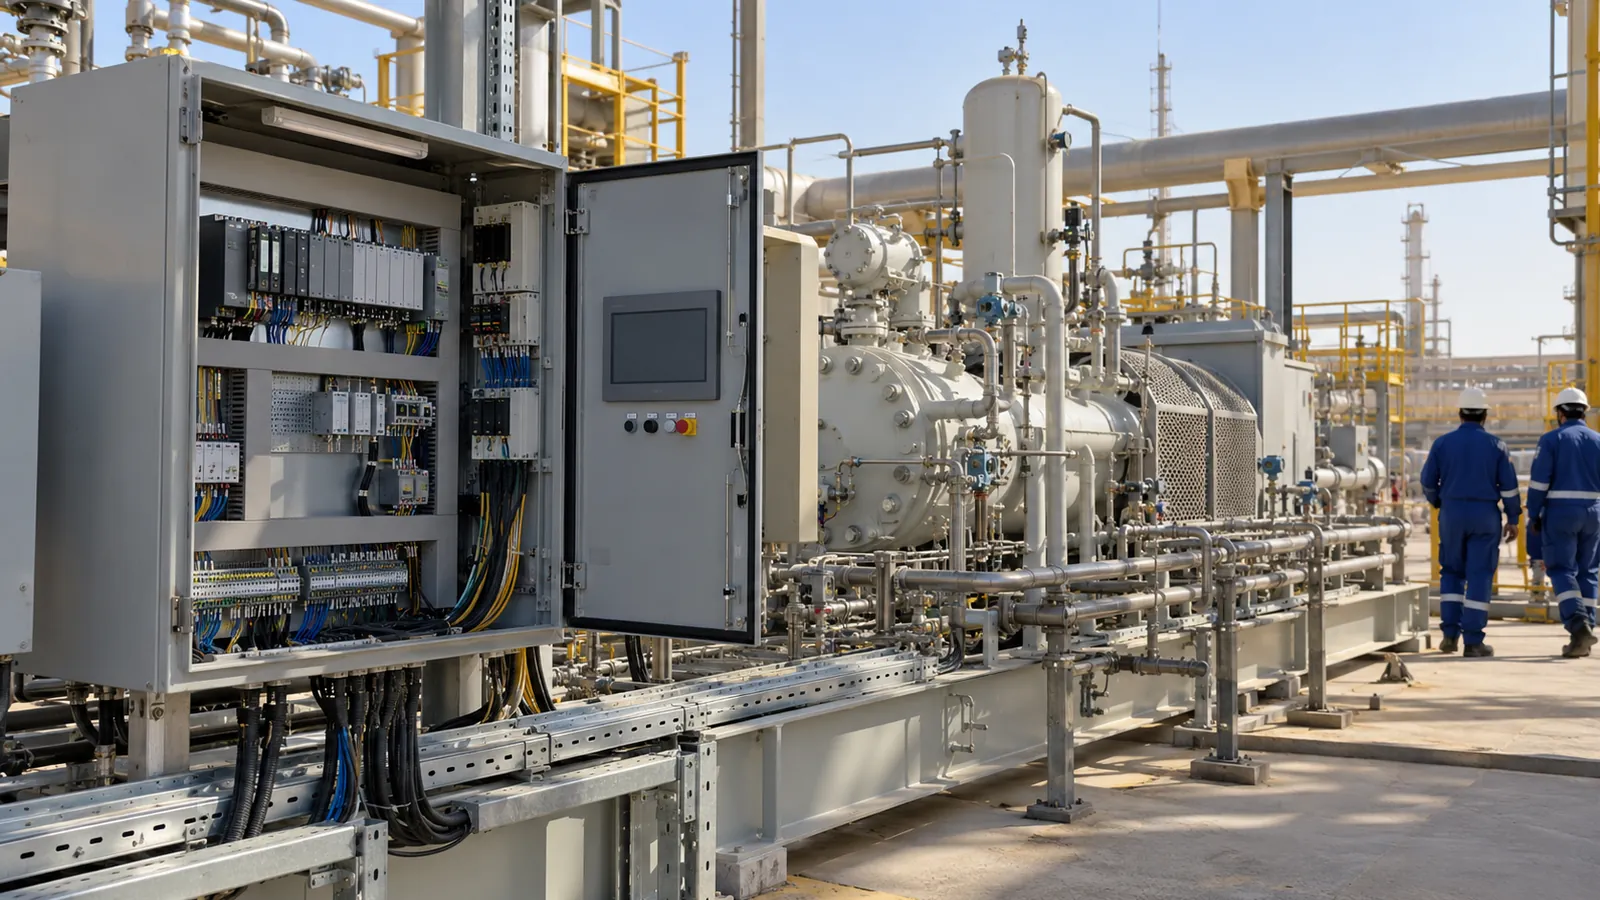
It starts, loads, unloads and protects the machine, and keeps the discharge pressure inside its band. The PLC checks that every start permissive is healthy, runs the starting sequence, then adjusts capacity as demand changes. If a protected value leaves its limit, the system alarms or trips in the order the machine requires.
The logic we write for a compressor or a compressor group includes:
- start permissives: oil level and temperature, cooling, suction and discharge conditions, and drive readiness;
- load, unload and modulating control against a pressure band or flow demand;
- trip and alarm handling for temperature, pressure, motor current and motor status, each with a first-out indication;
- sequencing of several compressors, so lead and lag machines rotate and the smallest combination that meets demand runs; and
- hand-over to a standby machine on trip, with the operator told which one took over and why.
Where the compressor manufacturer supplies a dedicated controller for the machine itself, we keep it in charge of machine protection and integrate its status into plant control instead of duplicating it.
Compressor control system: what we deliver
| Item | Scope / platform | Standard | Typical duration |
|---|---|---|---|
| Compressor PLC logic | Siemens S7-1200/1500, Rockwell CompactLogix, Schneider Modicon M340/M580 or ABB AC500 | IEC 61131-3 | 2–6 weeks per system |
| Local HMI | Machine overview, set-points, alarm history and run hours | ISA-101 where specified | 1–4 weeks |
| Multi-machine sequencing | Lead, lag and standby rotation with pressure-band control | Project functional description | Included in PLC programming |
| Plant integration | Modbus TCP, Profinet, Ethernet/IP or OPC UA to plant SCADA or DCS | IEC 62443 basics for networks | 3–8 weeks |
| FAT, SAT and loop checks | Skid-side test, then site commissioning and performance run | Client or packager ITP | Per project schedule |
We programme on Siemens, Rockwell, Schneider and ABB platforms and build with ABB, Schneider Electric and Siemens components.
How do skid packagers and OEMs work with an outside controls engineer?
They send us the skid's P&ID, I/O list and control narrative, and we deliver tested software before the skid leaves the yard. For the packager, that means one less specialist to hire for a single project. For the end user, it means the skid behaves the same way as every other skid on the site, because the interface to the plant system follows a set standard.
We agree early on three things: the tag structure and naming, the communication points the plant system needs, and the alarm priorities. We then test the full skid logic against simulated inputs, and again with the real skid during the packager's own FAT. A witnessed test by the end user is welcome. On site, the work shrinks to loop checks, the interface test with the plant system and the performance run. Our PLC programming services page describes the platforms in detail.
Can one control system run several compressors efficiently?
Yes. A sequencer reads the header pressure, knows each machine's capacity and chooses the combination that holds the pressure with the least waste. Machines wear evenly because the lead role rotates by run hours. Short cycling is limited by minimum run and minimum stop timers, and a stuck machine is skipped automatically.
The compressed-air or gas network is also monitored: header pressure, dryer status, receiver levels and flow. Operators see which machines are running, how loaded each is, and which alarms are active. For energy reporting, see energy monitoring systems.
How is a compressor or skid control project delivered?
- Enquiry. You or the packager send the P&ID, I/O list and control narrative.
- Review. We check the narrative for gaps, such as undefined trip actions or missing permissives, and agree answers with you.
- Design. We issue the software design, tag list and communication map for approval.
- Programming. We write PLC logic and HMI screens to the approved design.
- Factory acceptance test. We test the logic against simulated signals, then at the skid with your witness if you wish.
- Site acceptance. We carry out loop checks, interface tests and a performance run. See control system commissioning.
- Documentation. You receive source code, backups, I/O lists and operating notes.
- Support. We remain available for modifications and fault call-outs.
Who we build compressor and skid controls for
KSA Industrial Automation Company has worked in Saudi Arabia since 1995 and is approved by Saudi Aramco, SABIC and the Royal Commission for Jubail and Yanbu. We have carried out projects for all three, under systems certified to ISO 9001, ISO 14001 and ISO 45001.
Our customers include plant owners with compressed-air and process-gas duties, and packagers who need a controls engineer for a skid they are building. Typical skids include chemical injection, metering, filtration, water treatment and utility packages. We are based in Al Shati District, Dammam, and we take projects in all regions of Saudi Arabia. Our DCS integration page explains how skids connect to larger control systems.
Common questions before you request a quotation
Who provides a compressor control system in Saudi Arabia?
KSA Industrial Automation Company provides PLC logic, HMI and plant interfaces for compressors, for plant owners and skid packagers, from logic design to commissioning. We have worked on projects for Saudi Aramco, SABIC and the Royal Commission. We test at the packager's yard where required and support the system after handover.
What affects the cost of compressor controls?
Cost follows the number of machines, the I/O count, the PLC platform, whether the OEM controller is retained, the sequencing requirement, the plant communication interface, the witnessed test requirement and the documentation package. A control narrative and I/O list let us price these against your specification.
How long does compressor control programming take?
A single skid is typically programmed within a few weeks, followed by factory and site testing. Multi-compressor plants and projects with several interfaces take longer. Clear control narratives and quick approval of the software design shorten the schedule more than anything else.
Can you replace the controller on an existing compressor?
Yes. We record the existing logic and I/O, write and test the replacement offline, then cut over in a planned shutdown. Protection functions are proved by simulated trips before the machine is released, and the old controller stays available until the new one has run reliably.
Do you work with the compressor manufacturer's own controller?
Yes. Where the manufacturer's controller stays in charge of the machine, we integrate its status, alarms and set-points into your plant control over its supported protocol, and we leave its protection logic as designed by the manufacturer.
What should I send to get a quotation?
Send the P&ID, I/O list, control narrative and details of the plant system the skid connects to. For existing machines, add the controller make and a photo of the control panel. Your proposal then sets out scope, standards, duration and price.
Building or upgrading a compressor control system in Saudi Arabia? Send the P&ID and control narrative; our quotation reaches you within one working day. Email: inquiry@ksaindustrialautomation.com | Request a quotation