KSA Industrial Automation Company provides PLC programming services in Saudi Arabia for process plants, utilities and machine builders, working on Siemens, Rockwell, Schneider and ABB controllers. We write the control logic against your functional description, prove it on a simulated I/O rig, and hand over a commented, backed-up program that your own engineers can maintain.
What you receive: a written proposal with the scope, controller platform, deliverables and programme within one working day of receiving your I/O list, P&IDs or functional description. Request a quotation
PLC programming services: what we deliver
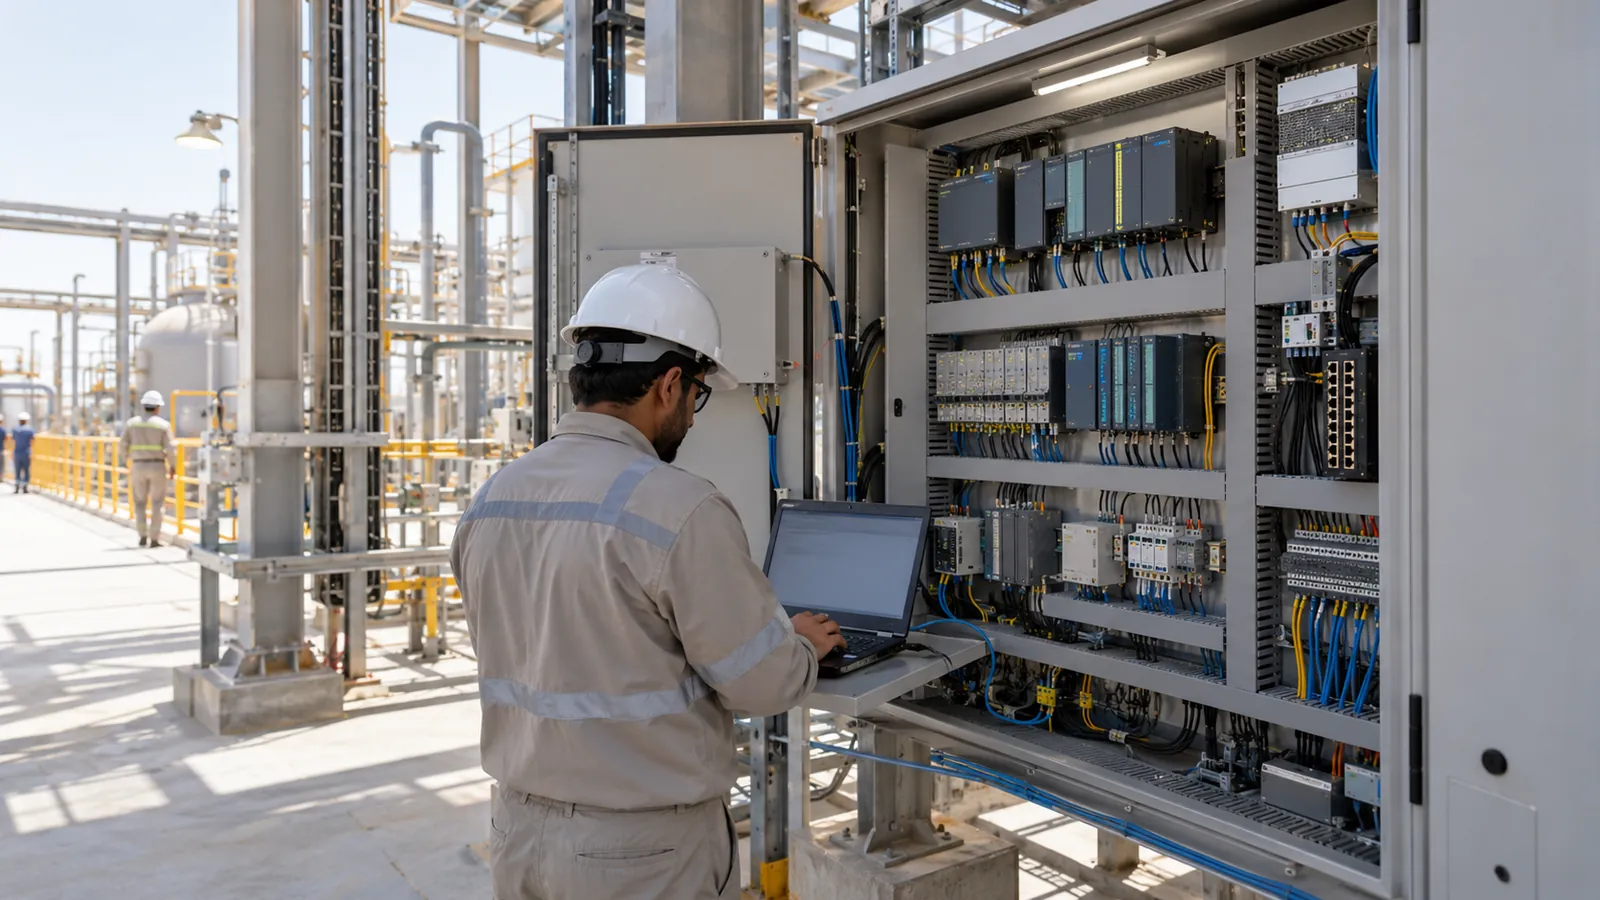
A PLC program is more than ladder rungs. We deliver the structure around it: a functional design specification, tag and I/O database, the controller code, the HMI tags it exposes, and the test evidence that proves it. The table sets out the platforms and typical durations.
| Item | Platforms / range | Standard | Typical duration |
|---|---|---|---|
| Siemens PLC programming | S7-1200/1500 in TIA Portal; S7-300/400 | IEC 61131-3 | 2–6 weeks per system |
| Rockwell PLC programming | ControlLogix and CompactLogix in Studio 5000 | IEC 61131-3 | 2–6 weeks per system |
| Schneider PLC programming | Modicon M340 and M580 | IEC 61131-3 | 2–6 weeks per system |
| ABB PLC programming | AC500 | IEC 61131-3 | 2–6 weeks per system |
| Functional design specification | Sequences, interlocks, alarms and modes of operation, issued for your approval | ISA-88 terms where batch logic applies | Included in the programme |
| Software factory acceptance test | Logic tested against simulated I/O with a signed test record | Your ITP or ours | Per project schedule |
Duration depends on the number of I/O points, the number of drives and valves, and how quickly you approve the functional design. A skid with 200 I/O sits at the short end; a multi-unit plant with batch sequences sits at the long end.
What are the 5 PLC languages?
The five languages in IEC 61131-3 are ladder diagram, function block diagram, structured text, sequential function chart and instruction list. We choose the language to fit the task, not the habit. Ladder suits discrete interlocks that a maintenance technician must read at 2 a.m. Structured text suits calculations, recipes and array handling. Function blocks suit analogue loops and reusable equipment modules. Sequential function charts suit start-up and shutdown sequences. Instruction list is deprecated, and we do not use it on new work.
Which software is used for PLC programming?
The right software is the one that matches the controllers you already run. Siemens controllers are programmed in TIA Portal, Rockwell controllers in Studio 5000 Logix Designer, Schneider Modicon controllers in EcoStruxure Control Expert, and ABB AC500 in Automation Builder. Mixing platforms inside one plant raises spares, training and licence cost, so we recommend extending your installed platform unless a project reason points elsewhere. For a new plant with no standard, we compare the platforms on your I/O count, networking and local support.
How is a PLC program written, tested and handed over?
- Enquiry. You send the I/O list, P&IDs or a functional description, plus any existing program.
- Site data. We confirm the controller family, firmware, network topology and any plant standards for naming and alarms.
- Functional design. We issue the functional design specification with the control narrative, interlock matrix and alarm list for your approval.
- Programming. The code is built in structured, reusable blocks, with one block per equipment type and commented networks.
- Software FAT. We run the logic against a simulation of your I/O, force each fault condition, and record the results.
- Site commissioning. We load the program, check each signal from field to controller, and tune loops and timers under process conditions.
- Documentation. You receive the commented source, an offline backup, the I/O and tag database, and the test record.
- Support. Remote support is available after handover, and we offer a modification service as your process changes.
For the step that follows programming, read our control system commissioning page, which sets out the site-side FAT, SAT and handover work.
Who we write PLC programs for
KSA Industrial Automation Company has worked in Saudi Arabia since 1995 and is approved by Saudi Aramco, SABIC and the Royal Commission for Jubail and Yanbu. We have worked on projects for all three, and our quality, environmental and safety management systems are held to ISO 9001, ISO 14001 and ISO 45001.
Our PLC work covers pump stations, water treatment, tank farms, compressor skids and packaging lines, as well as retrofits of ageing controllers. If your project is brand-specific, see our Siemens TIA Portal programming, Rockwell integration or Schneider PLC integration pages, and pair the controller with an HMI built to the same alarm philosophy. We take projects in every region of Saudi Arabia, from our base in Dammam. Emergency PLC support is available remotely the same day and on site within one working day in the Eastern Province.
PLC programming questions
Who provides PLC programming services in Saudi Arabia?
KSA Industrial Automation Company provides PLC programming services in Saudi Arabia from its Dammam base, on Siemens, Rockwell, Schneider and ABB controllers. We have been active since 1995 and have worked on projects for Saudi Aramco, SABIC and the Royal Commission.
What affects the cost of PLC programming?
Cost follows the number of I/O points, the number of equipment types, the complexity of sequences and interlocks, the controller platform, the level of documentation required, and the testing your inspection plan demands. Reusing proven blocks lowers effort. Send the I/O list and the proposal prices each of these against your scope.
How long does PLC programming take?
Most systems take two to six weeks of programming. The range depends on I/O count, sequence complexity and how quickly you approve the functional design. Software testing adds time at the start but removes most of the commissioning risk, so we plan it into the programme rather than treating it as optional.
Can you modify a PLC program written by someone else?
Yes. We take a backup, review the structure, document what each block does, and then make the change in a controlled way. If the original source is missing, we reconstruct a working copy from the controller. You receive the updated source and a change record.
Can you work to our consultant's specification?
Yes. We read your consultant's control narrative, I/O schedule and cause-and-effect charts, raise clarifications before programming starts, and issue the functional design specification for approval. Deviations are listed in writing so that your consultant sees every change.
What should I send to get a quotation?
Start with the I/O list and whichever of the P&IDs or a process description you have. For an existing program, add the controller type and a backup. We confirm the platform, scope and programme, and issue the quotation within one working day.
Looking for PLC programming services in Saudi Arabia? Tell us the controller platform and the I/O count, and a priced scope reaches you within one working day.
Email: inquiry@ksaindustrialautomation.com | Request a quotation