KSA Industrial Automation Company delivers Allen-Bradley PLC programming in Saudi Arabia for ControlLogix and CompactLogix controllers, with FactoryTalk View screens and EtherNet/IP networks. We are an authorised Rockwell Automation partner for Allen-Bradley systems. Every project is written in Studio 5000, tested against simulated I/O, and commissioned so that the plant keeps running after we leave.
What you receive: a written proposal with the controller family, firmware, software versions, deliverables and programme, issued within one working day of receiving your I/O list, P&IDs or existing .ACD file. Request a quotation
Allen-Bradley PLC programming with Studio 5000
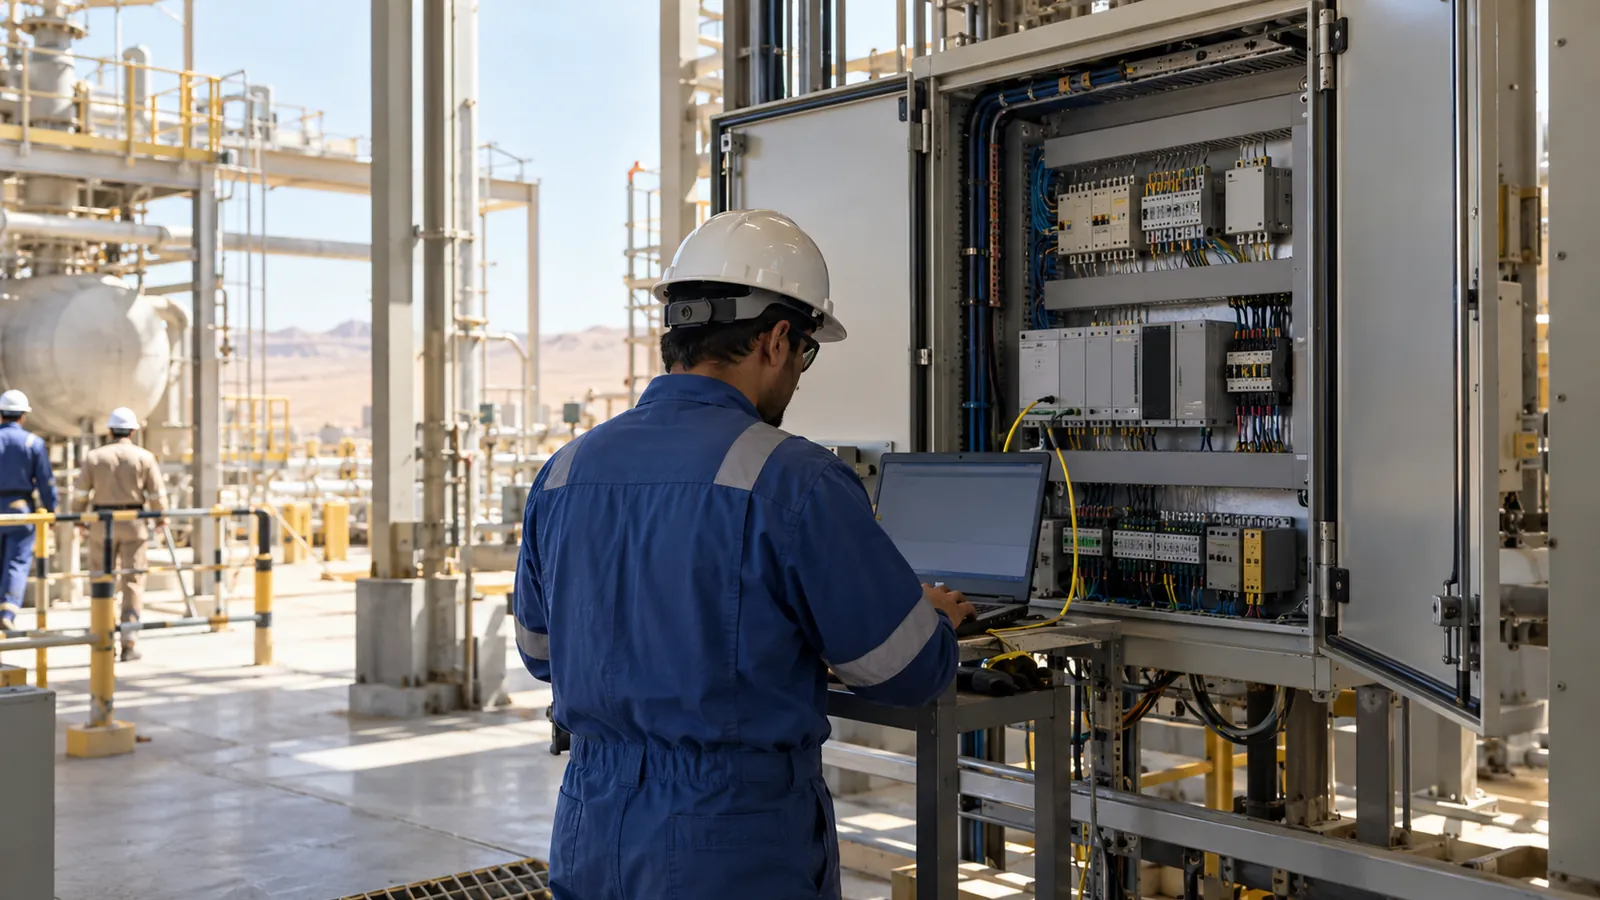
Many Saudi sites, especially packaging, food and some oil and gas facilities, run Rockwell controllers. They need engineers who can read and extend an existing Logix project as well as build a new one. We act as a Rockwell system integrator for both cases, starting from the hardware you have installed and not from a platform preference.
| Item | Platforms / range | Standard | Typical duration |
|---|---|---|---|
| Controller programming | ControlLogix and CompactLogix in Studio 5000 Logix Designer | IEC 61131-3 | 2–6 weeks per system |
| HMI commissioning | FactoryTalk View, including PanelView Plus terminals | ISA-101 principles | 1–4 weeks |
| SCADA | FactoryTalk supervisory software | ISA-18.2 where relevant | 4–12 weeks |
| Networks | EtherNet/IP, device-level ring and managed switch configuration | ODVA EtherNet/IP specification | Included in the programme |
| Drives | PowerFlex drives and I/O over EtherNet/IP with Add-On Profiles | Manufacturer guidelines | Per drive count |
| Software FAT | Logic tested against simulated I/O with a signed record | Your ITP or ours | Per project schedule |
What programming software does Allen-Bradley use?
Rockwell programs its Logix controllers in Studio 5000 Logix Designer, which supports ladder, function block, structured text and sequential function chart. The same tag database serves the HMI, so a change on the controller is visible on the screen without re-mapping addresses. FactoryTalk View Studio builds the operator screens, and Connected Components Workbench covers smaller Micro800 controllers.
Each package needs a licence, which plants normally hold on their own engineering laptops. We work on your licence, check the firmware revision against the software version and deliver the project file with an offline backup.
How do I connect an HMI to an Allen-Bradley PLC?
Put both on the same EtherNet/IP network, give each a fixed address, and add the controller as a data source in FactoryTalk View. The screen then reads and writes tags in the controller directly. For a PanelView Plus terminal, the application is built in FactoryTalk View Studio, downloaded to the terminal and tested tag by tag.
We keep the address plan in a single table, set the communication timeout so that a broken cable raises a clear alarm, and test the failure case during commissioning. The communication protocol behind all of this is EtherNet/IP, which carries both control data and diagnostics.
How do we program and integrate a Rockwell system?
- Enquiry. You send the I/O list, P&IDs or the existing Studio 5000 project.
- Site data. We confirm the controller family, firmware revision, network layout and drive types.
- Design. A functional design sets the program structure, tag naming and interlock list.
- Programming. Add-On Instructions are built once for each motor, valve and loop, so behaviour is identical wherever they are used.
- Software test. The program runs with emulated I/O, faults are injected and each result is recorded.
- Site commissioning. We download to the controller, check each signal and tune loops and drives under process conditions.
- Documentation and support. You receive project files, an offline backup, the tag and I/O list and the test record.
Older PLC-5 and SLC 500 systems follow the route described under PLC retrofit and upgrade, and the supervisory layer sits under SCADA integration.
Where we deliver Rockwell controller work
Our company has worked in Saudi Arabia since 1995 and is approved by Saudi Aramco, SABIC and the Royal Commission for Jubail and Yanbu. We have worked on projects for Marafiq in Jubail and for Saudi Aramco in Riyadh.
Three situations bring us in most often. A new line or skid built around CompactLogix where the machine builder has left no time for software. An ageing system that needs a current controller. A ControlLogix plant that wants more screens, a historian or a supervisory layer. For the brand-neutral view, see our HMI development page. We take Rockwell projects in every region of Saudi Arabia.
Allen-Bradley partner questions
Who provides Allen-Bradley PLC programming in Saudi Arabia?
KSA Industrial Automation Company provides Allen-Bradley PLC programming in Saudi Arabia from its engineering office in Dammam. We cover ControlLogix and CompactLogix in Studio 5000, FactoryTalk View screens, PowerFlex drive integration and EtherNet/IP networks, and we attend sites in every region.
Who is a distributor for Allen-Bradley in Saudi Arabia?
KSA Industrial Automation Company provides the engineering, not the stock. Distributors handle orders, delivery and warranty, while we program, integrate, test and commission the Rockwell hardware you have bought, whoever supplied it. We prepare the I/O list and parts list so that the right modules and licences are ordered once.
What affects the cost of Allen-Bradley HMI commissioning and programming?
Price follows the I/O count, the controller family, the number of drives and networked devices, the extent of sequence logic, the HMI scope and the testing in your inspection plan. A clear I/O list and an agreed naming convention reduce effort. Send both and the proposal prices each factor.
How long does Rockwell controller programming take?
Most Rockwell systems take two to six weeks of programming, FactoryTalk View screens add one to four weeks, and a supervisory layer adds four to twelve. I/O count, drive count and the speed of your approvals decide where a project sits in the range.
Can you take over a program written by another contractor?
Yes. We upload the program, open it in Studio 5000, document the routines and tasks, and then make changes in a version-controlled copy. If the source file is missing, we rebuild a working project from the controller and compare behaviour before modifying anything.
What should I send to get a quotation?
Send your I/O list, P&IDs and the Rockwell hardware list. If a program exists, add the Studio 5000 version and a backup file. We return a priced proposal that separates programming, screens and site commissioning.
Looking for Allen-Bradley PLC programming in Saudi Arabia? Send your I/O list and Rockwell hardware list, and a quotation reaches you within one working day. See all automation partners.
Email: inquiry@ksaindustrialautomation.com | Request a quotation