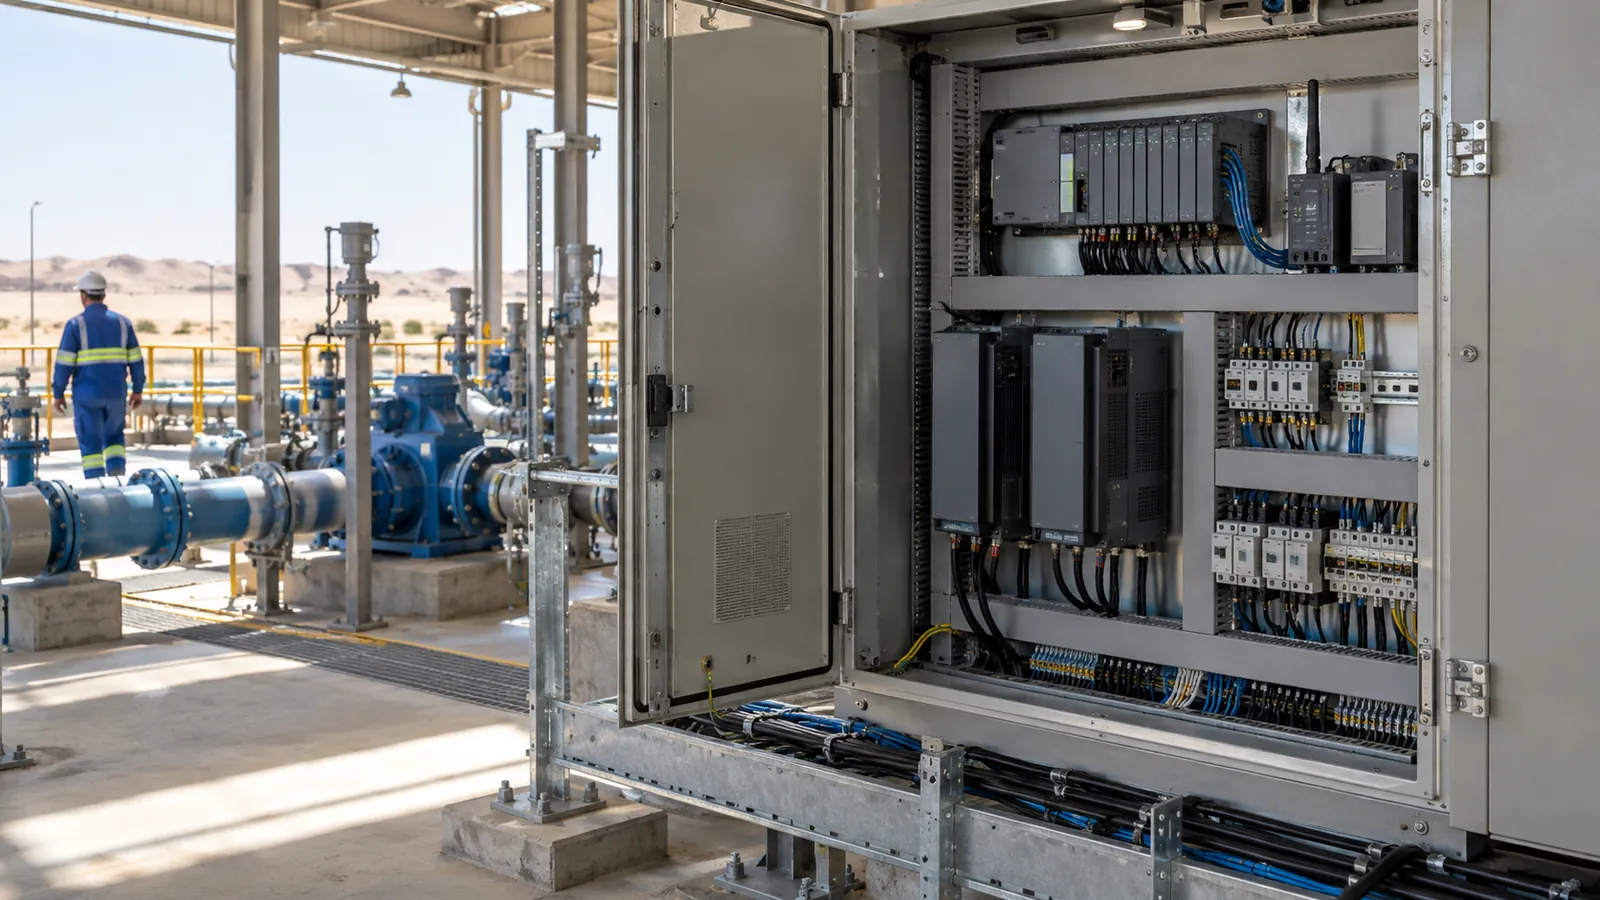
Pump station automation benefits fall into three groups: lower energy use, fewer unplanned visits and longer equipment life. Automatic duty rotation, variable-speed control and remote alarms reduce wasted running, catch faults before they become failures, and let one operator watch many stations. The size of each saving depends on your head, flows and run hours.
What you receive: send your station list, pump data and current alarm practice and we return a written automation proposal within one working day. Request a quotation
By Eng. Junaid Ali, KSA Industrial Automation Company. Published October 2026.
What do pump station automation benefits look like in practice?
Each benefit comes from a specific control function. The table links them so you can judge which apply to your stations.
| Function | What it does | Benefit |
|---|---|---|
| Duty and standby rotation | Alternates pumps by run hours or fault | Even wear; standby always proven |
| Level-based staging | Starts and stops pumps by tank or wet well level | Avoids overflow and dry running |
| Variable-speed control | Matches speed to the flow or pressure demand | Lower energy at partial flow, softer starts |
| Protection logic | Trips on dry run, high temperature, overload | Fewer burnt motors |
| Telemetry and alarms | Sends status and faults to a central room | Fewer routine visits, faster fault response |
| Run-hour and start counters | Records operating history | Maintenance when needed, not by calendar |
How does automation cut energy use?
The main route is speed control. By the pump affinity laws, flow varies with speed, head with the square of speed, and power with the cube. A modest speed reduction therefore gives a larger power reduction, provided the system does not depend on static head.
Other energy gains come from reduced starts, which cut inrush current, and from level setpoints that let pumps run at their efficient point instead of cycling. A pump that is throttled by a valve wastes the difference as heat. Replacing the valve with speed control returns that energy. Fewer starts also mean less stress on couplings, seals and starters, and a soft start reduces pressure surges in the pipework that otherwise cause water hammer and leaks. Where several pumps share a header, the control logic can add or drop pumps so that each runs near its rated duty point rather than all running part-loaded.
Worked example: a 55 kW pump at 80% flow
This is an example to show the method; real savings depend on the system curve. A 55 kW pump delivers full flow for part of the day and 80% of flow for the rest, in a system with no static head, so friction head follows the speed squared.
| Step | Calculation | Result |
|---|---|---|
| Speed for 80% flow | 80% of full speed | 0.8 |
| Power fraction by affinity law | 0.8 × 0.8 × 0.8 | 0.512 |
| Shaft power at 80% flow | 55 × 0.512 | about 28 kW |
| Reduction against full-speed running | 55 − 28 | about 27 kW |
The ideal reduction is 27 kW, or about 49%. If the station has static head, the saving is smaller, and drive and motor losses reduce it further, so the proposal calculates it from your pump curves. Over 4,000 hours at 80% flow, 27 kW equals about 108,000 kWh. Treat that as the upper bound for a pure friction system.
How does automation cut callouts?
A callout is a vehicle trip to a station to check a fault or a routine reading. Remote monitoring replaces most of these.
Take six stations, each visited twice a week by routine round. That is 12 visits a week, or 624 a year. If telemetry shows pump status, level, pressure, run hours and alarms, routine rounds move to a fortnightly or monthly check, and visits happen for real faults only. Even a reduction to one visit per station per fortnight leaves about 156 visits a year, a fall of 75%. The saving in fuel, time and exposure to summer heat is real, though the figure depends on your rounds.
The data also tells you why a pump stopped: overload, dry run or power loss. The technician arrives with the right spare, instead of a general toolbox. Trend data helps too: a rising motor current over weeks points to a worn bearing or a partly blocked impeller, and the visit can be planned before the pump trips. Run-hour counters let you balance duty between pumps so that both wear evenly, and they give maintenance a factual basis for overhaul dates.
What does a pump station automation project include?
- Site survey: pumps, motors, level devices, power and communications.
- Control philosophy: duty rules, level setpoints, alarms, fallback.
- PLC or RTU programming and drive set-up.
- Telemetry link: 4G, fibre or radio, with a SCADA or cloud dashboard.
- Factory test on a bench, then site test with the pumps.
- Handover with drawings, backups and operator training.
RTU, telemetry and IIoT projects typically take 3–8 weeks. KSA Industrial Automation Company works on projects for Saudi Aramco, SABIC and the Royal Commission for Jubail and Yanbu. Our pump station automation page describes the scope we deliver, with RTU and telemetry and remote monitoring and IIoT covering the communications.
Common questions about pump station automation benefits
What is the main benefit of automating a pump station?
The main benefit is reliable operation with less manual effort: pumps start and stop on level, standby pumps take over on failure, and faults reach the right person quickly. Energy and maintenance savings follow from that control.
Does a variable-speed drive always save energy?
Not always. Savings are largest where flow demand varies and friction dominates the system. Where static head is high or the pump runs at full flow most hours, savings are small. We calculate it from your duty profile.
What does pump station automation cost?
Cost depends on the number of pumps and stations, drive and PLC or RTU hardware, level instruments, communication method, SCADA licences, testing and site conditions. A proposal from your pump data shows each element and the payback assumptions.
Can an existing pump station be automated without replacing the pumps?
Yes. We keep the pumps and motors and upgrade starters, controls, instrumentation and communications where needed. Existing electrical condition is surveyed first, so we know what can be reused safely.
How are alarms delivered to the operator?
Alarms go to the SCADA screen and, where specified, to phones by SMS or email with escalation to a second person if nobody acknowledges. Alarm priorities are set so that minor events do not wake anyone.
Want to see which pump station automation benefits apply to your stations? Send your station list and pump data and receive a quotation within one working day. Email: inquiry@ksaindustrialautomation.com | Request a quotation