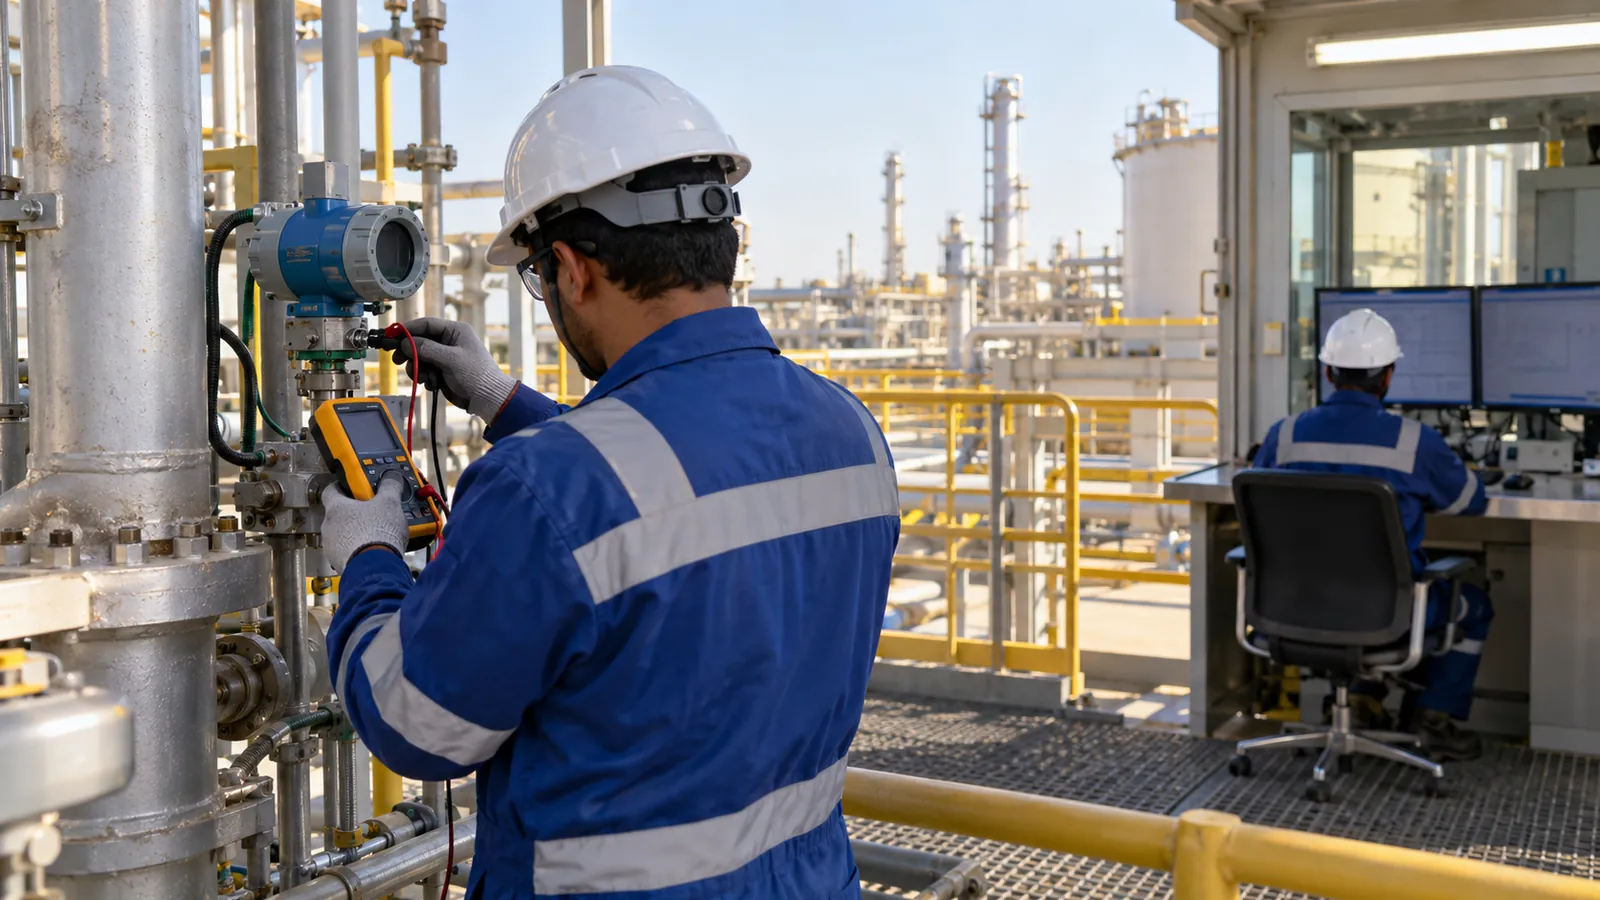
A loop check procedure proves that each instrument loop works end to end, from the field device through the wiring and I/O card to the value and alarm on the control screen. The loop folder holds the paperwork for that proof: loop diagram, datasheet, calibration record, test sheet and sign-off. One folder is kept for every loop.
What you receive: send your I/O list, P&IDs or loop diagrams and we return a written proposal for the loop checks within one working day. Request a quotation
By Eng. Junaid Ali, KSA Industrial Automation Company. Published October 2026.
What does loop check mean?
A loop is one measurement or control path: a transmitter, its cable, a junction box, a marshalling terminal, an input or output card and the tag in the PLC or DCS. "Checking" it means testing the whole chain with a known signal and confirming the response at the far end. A loop check is not a calibration of the instrument alone, and it is not a logic test, although all three are linked.
The result is a signed record per loop, so that plant owners can show the system was proved before start-up.
What does a loop folder contain?
The contents follow the project specification, and the usual set is below.
| Document | Purpose |
|---|---|
| P&ID extract | Shows the loop's place in the process |
| Loop diagram | Wiring from field device to I/O channel, with terminal numbers |
| Instrument datasheet | Range, units, tag, service and power |
| Calibration certificate | Proves the instrument was set against a reference |
| I/O list line | Links the field tag to the PLC or DCS address |
| Loop check sheet | The test steps, results and signatures |
| Cause and effect or interlock extract | Shows which trips or alarms use the signal |
| Punch list | Open points with owner and closure date |
We prepare loop folders to ISA and IEC practice and the project's inspection and test plan.
How is a loop check procedure carried out?
The steps below suit a transmitter loop. Valves and switches follow the same pattern.
- Confirm the folder is complete and the drawings are the latest revision.
- Check the wiring: continuity, polarity, insulation where specified, shield earthed at one end.
- Power the loop and confirm the loop supply voltage at the transmitter.
- Inject or simulate the signal at the field end, stepping through 0%, 25%, 50%, 75% and 100% of range.
- At each point, read the value on the control screen and compare with the expected value.
- Test alarms and trips: raise the signal past each setpoint and confirm the alarm text, priority and interlock action.
- For control valves, stroke the valve and confirm position feedback in both directions.
- Sign the sheet, record any fault on the punch list and re-test after repair.
Worked example: a 0–5 m level transmitter on a 4–20 mA loop
This is an example to show the method; ranges differ. The transmitter measures 0 to 5 m of level. At 4 mA it reads 0 m and at 20 mA it reads 5 m. The control system tolerance is ±0.5% of span, which is ±0.025 m.
| Test point | Injected current | Expected level | Reading accepted between |
|---|---|---|---|
| 0% | 4 mA | 0.00 m | −0.025 to 0.025 m |
| 25% | 8 mA | 1.25 m | 1.225 to 1.275 m |
| 50% | 12 mA | 2.50 m | 2.475 to 2.525 m |
| 75% | 16 mA | 3.75 m | 3.725 to 3.775 m |
| 100% | 20 mA | 5.00 m | 4.975 to 5.025 m |
The expected value follows the formula level = (mA − 4) ÷ 16 × 5. At 12 mA that is 8 ÷ 16 × 5 = 2.5 m. If the screen shows 2.31 m, the error is 0.19 m, or 3.8% of span, well outside tolerance, so the technician checks scaling in the PLC before suspecting the instrument. The high alarm set at 4.0 m is then tested by injecting 17 mA, which is exactly 4.0 m.
What goes wrong most often during a loop check?
Four faults cause most failed loops:
- Wrong scaling in the PLC, for example 0–100 entered for a 0–5 m range.
- Reversed polarity or a swapped pair, so the signal reads below 4 mA.
- Shield or earthing faults that add noise to the reading.
- Mislabelled tags, so the right signal appears on the wrong screen tag.
Finding these early is why we run loop checks before the process is introduced. Record every failure with the tag, the symptom and the fix, because patterns across loops, such as one junction box with several faults, point to a root cause. A loop that fails with water or air in the line is simpler than one that fails with product in it.
KSA Industrial Automation Company has carried out instrumentation and control work on projects for Saudi Aramco, SABIC and the Royal Commission for Jubail and Yanbu. Our loop checking and instrumentation service runs the sheets, and the results feed control system commissioning. If scaling errors point to the program, the PLC programming team corrects them.
Common questions about the loop check procedure
What is the difference between a loop check and calibration?
Calibration sets and verifies the instrument against a reference standard. A loop check proves the complete signal path, including wiring, I/O channel, scaling and the screen. Both are needed, and the calibration certificate goes into the loop folder.
Who performs and witnesses a loop check?
An instrument technician or commissioning engineer injects the signal, while a second person reads the control system. The client or consultant witnesses the sample or the full set, as the inspection and test plan states.
How many loops can be checked in a day?
A pair of technicians typically checks only a modest number of loops per day, and the figure depends on access, loop type, distance between field and control room, and whether radios or a second person are available. The plan states the rate.
Do we need to loop check every instrument?
Most specifications require 100% of loops, especially those with interlocks or alarms. For non-critical indicators, a sample may be agreed in the test plan. Safety-related loops are always fully tested.
What happens to the loop folders after start-up?
They are handed over with the as-built drawings, calibration records and punch list closure. Maintenance uses them as the baseline for future calibration and troubleshooting, so keep them in a controlled, searchable archive.
Need a loop check procedure run or loop folders compiled? Send your I/O list, P&IDs or loop diagrams and receive a quotation within one working day. Email: inquiry@ksaindustrialautomation.com | Request a quotation